English
- English
- Afrikaans
- беларускі
- Hrvatski
- lugha ya Kiswahili
- ქართული
- Кыргыз тили
- Монгол хэл
- IsiXhosa
- Somali
- O'zbek
- Hawaiian
- Հայերեն
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- tiếng Việt
- Italiano
- Nederlands
- ภาษาไทย
- Polski
- 한국어
- Svenska
- magyar
- Malay
- বাংলা ভাষার
- Dansk
- Suomi
- हिन्दी
- Pilipino
- Türkçe
- Gaeilge
- العربية
- Indonesia
- تمل
- ελληνικά
- український
- فارسی
- български
- ລາວ
- Latine
- Қазақша
- Azərbaycan
- Македонски
- Lietuvos
- Română
- Srpski језик
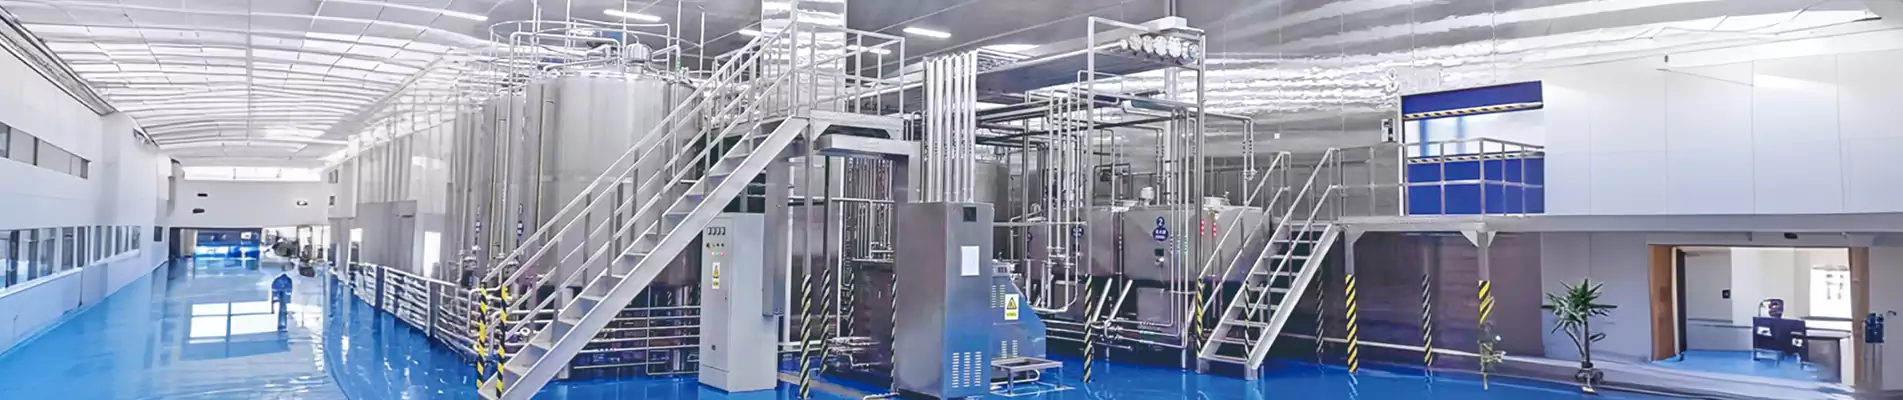


UHT Milk Production Line
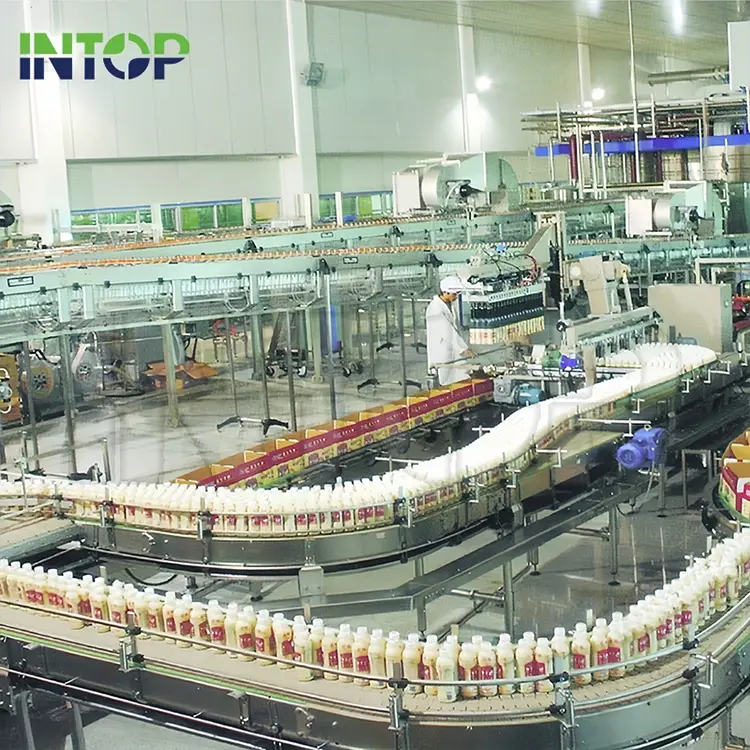
INTOP has extensive experience in UHT milk production line design, and the equipment manufactured by our factory has received consistent praise from customers both domestically and abroad. UHT milk has a long shelf life, can be transported over long distances at room temperature, and can be stored for extended periods without refrigeration.
Process Flow
Acceptance of Raw Milk → Clarification → Milk Cooling and Storage → Pre-Sterilization (15 mins) → Deaeration → Homogenization → UHT Sterilization → Aseptic Filling
INTOP can help you to design the UHT Milk production line from A to Z, and provide you with relevant equipment.
1. The purpose of raw milk purification is to remove mechanical impurities and reduce the number of microorganisms in the milk. Filtration purification can be used. Simple coarse filtration involves installing a filter screen on the milk receiving tank and covering it with multiple layers of gauze for filtration. The filter cloth should be cleaned and sterilized regularly. After purification, it is transported to a cooling tank, where the cooling temperature is 5℃~10℃ to inhibit bacterial growth. The number of microorganisms in the milk changes with the length of storage time and the level of temperature。
2. The raw milk is preheated and sterilized using pasteurization before homogenization. The purposes of pre-sterilization are:
(1) To initially kill most of the bacteria and pathogens, making UHT sterilization more thorough, ensuring food safety, and improving the storage stability of the finished product.
(2) To inhibit the activity of enzymes, so as to avoid adverse phenomena such as fat hydrolysis enzyme-catalyzed browning in the finished product. The sterilization temperature used is 80℃ for 15 min.
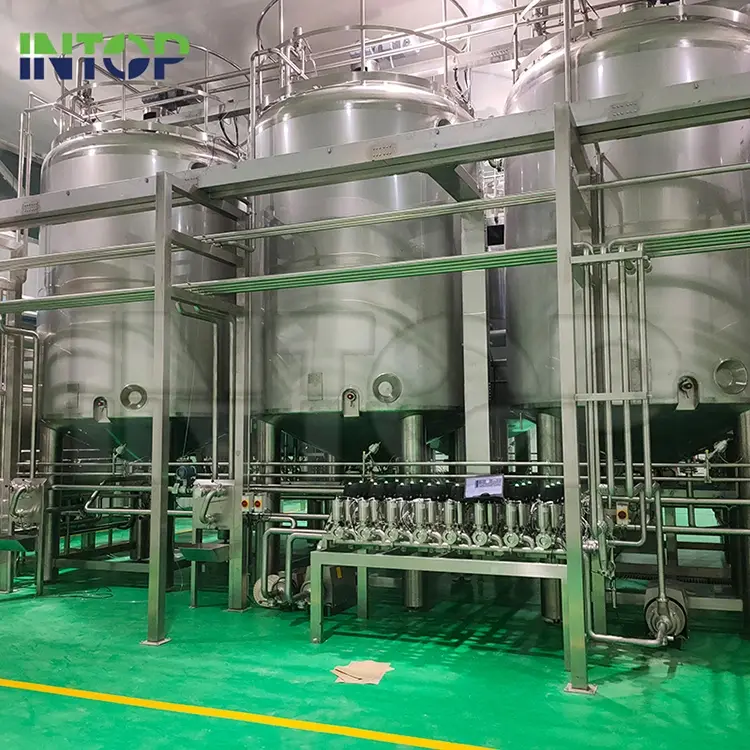
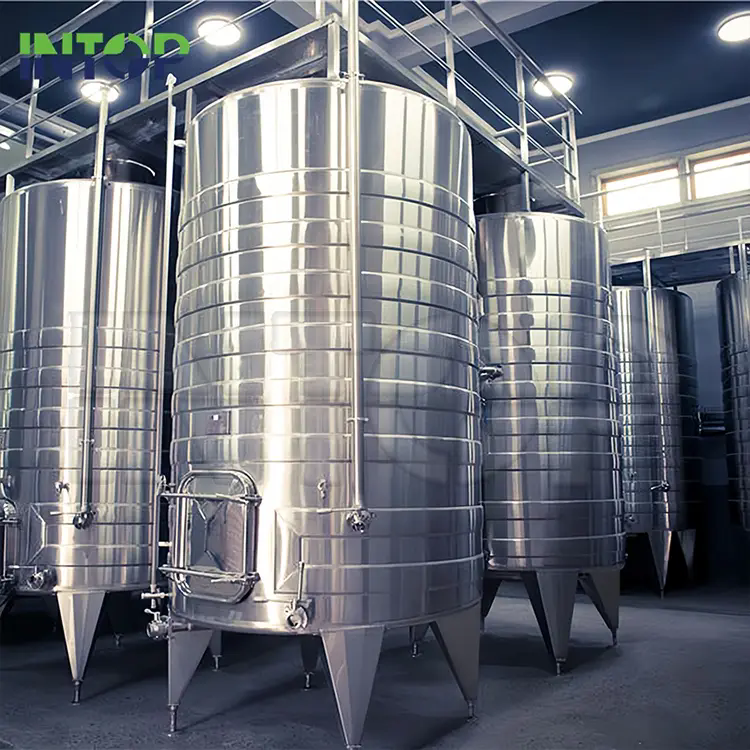
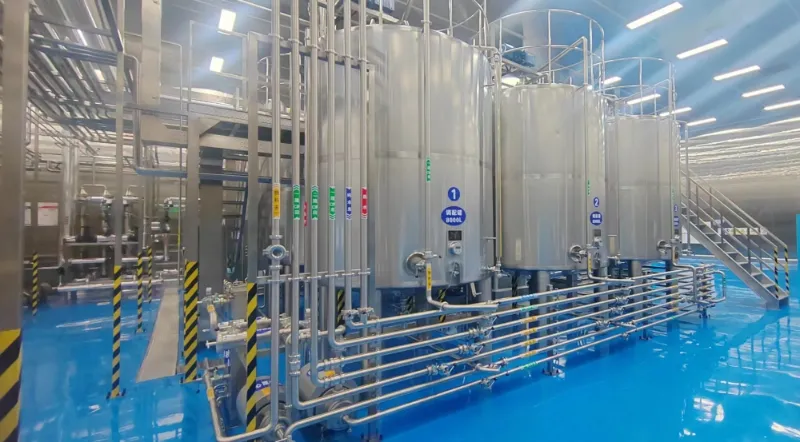
3. In order to ensure continuous production, several milk storage tanks are generally set up. The milk storage tank should be equipped with stirring to agitate the liquid regularly to prevent the fat from floating up and causing uneven distribution of raw milk components.
4.Higher temperature homogenization is beneficial to improve the effect, but too high a temperature will cause the denaturation of milk fat and milk protein. If the temperature is lowered and then homogenized, it will not only reduce the homogenization effect, but sometimes cause the fat globules to form cream grains. Therefore, the homogenization temperature of 55℃~80℃ and pressure of 2.0 MPa~2.5 MPa have better results.
5. Ultra-high temperature sterilization refers to heating the material through a heat exchanger to 135℃~150℃ in a continuous flowing state, and maintaining it at this temperature for a certain period of time to achieve commercial sterility. This method of sterilization maximizes the preservation of nutrients in the milk on the premise of effectively killing microorganisms, and the produced milk can be stored at room temperature for a long time.
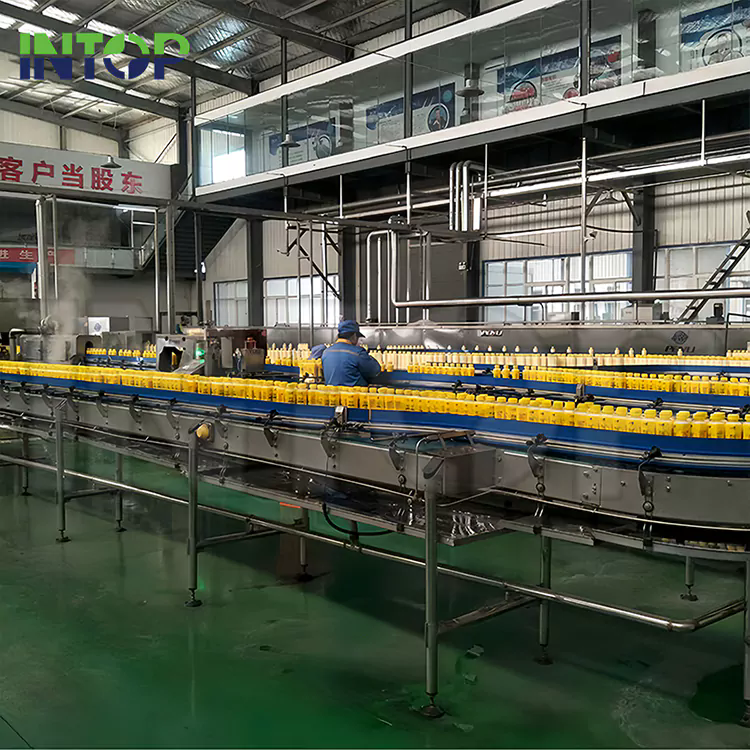
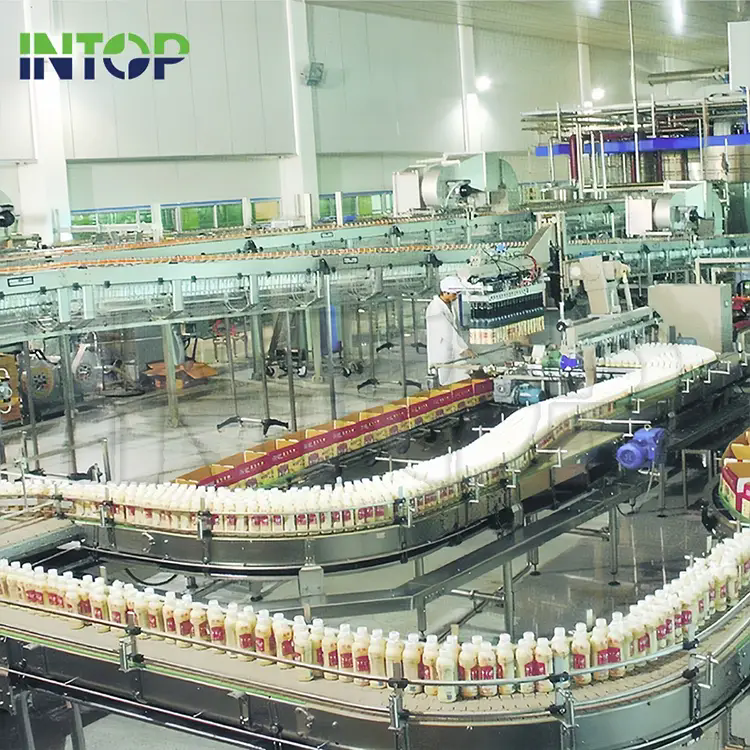
6. Aseptic Filling,Filling must be ensured to be carried out under sterile conditions.
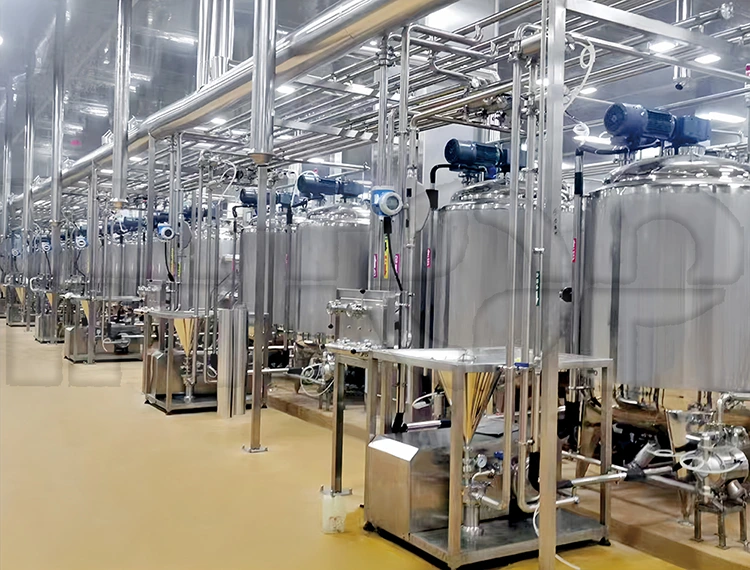
Intop has extensive experience in manufacturing UHT sterilized milk equipment. We have designed UHT milk production line and supplied equipment for countries such as Turkey, Saudi Arabia, Egypt, Sri Lanka, Australia, New Zealand, the United States, Kazakhstan, and others. If you have any technical questions or would like to discuss technical details, please contact us. Our technical team is available online to assist you.
Hot Tags: UHT Milk Production Line, UHT Milk Processing Equipment, Aseptic Filling Machine
Send Inquiry
Contact Info
-
Address
No. 266 Taibai Avenue, Huamei Intelligent Manufacturing Industrial New City, Zone A, Anlu City, Hubei Province, China
-
Tel
-
Email
For inquiries about Production Line, Juicing Machine and Water Treatment System or price list, please leave your email to us and we will be in touch within 24 hours.